- November 19, 2026
- by Almifthaah
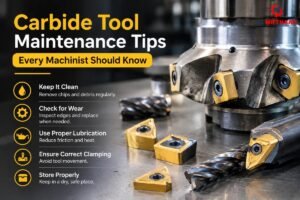
Carbide Tool Maintenance Tips Every Machinist Should Know
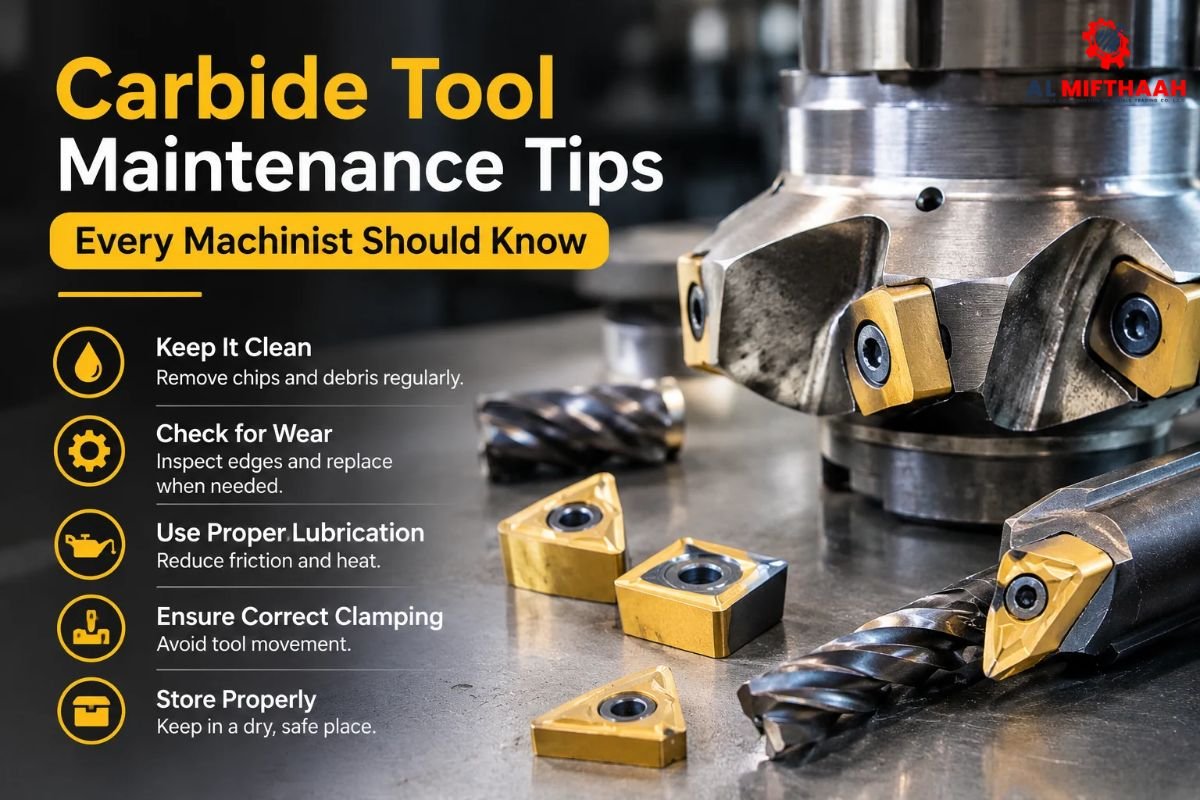
Although carbide tools are the foundation of modern machining, neglecting one’s tools can cause even the hardest cutting edges to wear prematurely. This guide covers carbide tool maintenance topics that all machinists should be aware of. This includes daily inspections, storage, cutting parameters, coolant usage, resharpening tools, as well as recognizing when to turn your tool.
By following these recommendations, you will be able to maintain the quality of your surface finishes, decrease the amount of scrap, and reduce your production costs. For a small job shop or large manufacturing plant, these steps carry some impact.
Table of Contents
ToggleKey takeaways
- Inspect and clean carbide tools every day, especially since many problems caused by hidden contaminants can be avoided.
- Keep tools in separate sleeves or racks to protect them from impact.
- Select speed and feed rate according to the material and the tool’s specifications, doing so gradually.
- Keep track of the wear and regrind counts of your tools so that you will be able to replace them on the basis of facts instead of speculation.
Why does carbide tool maintenance matter?
On the correct material, carbide is harder and more heat resistant than high-speed steel, and thus can run faster and longer. Gone is that benefit if the tool is not handled carefully, used at the wrong setting, or if it is not cleaned between jobs. Many stores consider carbide to be a consumable and will change it out as soon as it gets damaged. In practice, most cases of premature failures are due to preventable causes, including chipped edge due to poor handling, built-up edges due to incorrect speeds, and thermal cracking due to uneven coolant flow.
Therefore, a disciplined maintenance plan converts carbide from a cost to a resource. Tools provide consistent results from the first part to the last when operators are aware of what to do, what to avoid doing, and when to do it. This consistency is more important in tight tolerance pieces where a change in edge condition will move a dimension off spec. Good maintenance is then not a bonus job; it’s a job that goes into good parts.
How does tool wear affect production costs?
Carbide tools that are worn cause dimensional drift, rough surface finishes, and additional heat. All of these problems result in rework, scrap, and extra machine time, etc. Carbide is costly, and if a tool is replaced prematurely, money is lost; if it is used for too long, the workpieces may be damaged, and stress is put on the spindle. Maintenance that is consistent will keep each tool in the sweet spot between those two costs.
The cost of wear is also covered by wear. Sometimes a dull tool will cut, so operators will continue to use it and reduce the feed rate. With that slow cycle time, it adds up over hundreds of parts. Being able to monitor the lifespan of the tracking system per job and when wear starts allows you to use real data to plan when to replace the tracking system, rather than guess.
Understanding carbide tool types
Not every carbide tool will benefit from care in the same (equal) manner. Each solid carbide drill, indexable insert, and single point tool has various different geometries and consequently weak points. Knowing about these differences allows you to concentrate your inspection and maintenance efforts on the right places. A thin-flute tool will be much more sensitive to chip packing than a solid indexable insert.
Some shops may have multiple families of tools. A basic reference list of the common use and mode of failure of each tool is kept on the shop floor to minimise the amount of guessing. Operators can then identify a problem at an early stage, like a “notched edge” on a light finishing tool before it causes a problem in the workpiece.
Particular attention is warranted for milling processes, which have continuously varying cutting forces as the tool enters and exits the material. A well-known cutting and milling tools Dubai supplier often uses general catalogs to find the correct geometry for each job. The use of the right grade and geometry in the beginning makes maintenance easier later on.
| Tool Type | Typical Use | Main Maintenance Focus | Common Failure Mode |
| Single point tool | Turning, boring, facing | Edge inspection, insert seating | Edge chipping, nose wear |
| Indexable insert | General turning and milling | Clamp torque, pocket cleaning | Insert cracking, loose seating |
| Solid end mill | Slotting, profiling | Flute cleaning, runout checks | Flute packing, tip breakage |
| Solid drill | Hole making | Chip evacuation, coolant flow | Corner wear, thermal cracking |
Which carbide tools need the most care?
Tools with a thin, long, or small diameter require the most care, as these tools have less mass to absorb shock and heat. A single flute carbide endmill UAE user will often discover that a single flute will focus chip load, and chip clearance is crucial. Regularly inspect and use these tools with increased care when changing over. The heavier indexable tools are able to take rough handling but still have loose inserts and dirty pockets.
Keep in mind the sharpness of the cutting edge of the tool is its most important part, and consequently its most vulnerable part. Always protect the edge when unpacking and loading in the spindle.
Daily inspection and cleaning routines
Most problems are caught before they cost time with a short daily routine. Include inspection at the start of the shift and end-of-shift cleanup. Frequent tool inspection by operators is more likely to detect chips, cracks, and wear than when they only inspect when a part fails. Some minutes at the beginning of every day can save hours of troubleshooting.
Thoroughly clean tools before inspection. A chipped edge or a crack may be concealed with residual coolant, metal fines, or oil, and make a tool look better than it is. Additionally, use a dry lint-free cloth, and use a light solvent recommended for carbide where applicable. Do not use any abrasive pads, as they may scratch and create new stress points.
How to inspect carbide edges before each shift?
First, examine the cutting edge in appropriate lighting and, if it is small, with a magnifier. Check for chips, notches, and worn-out flank and rake faces. See if the edge is rounded at a sharp point; this may mean heat damage because it is rounded. Ensure that inserts fit flush in their pockets and clamp screws are not stripped or loose.
- Use a lint-free dry cloth to clean the tool and holder.
- Inspect the edge of the cutting tool under bright light; use a magnifier for small tools.
- Inspect flank faces for chips, cracks, and uneven wear patterns along with rake faces.
- Check for complete insertion and clamp screws torque.
- Take measurements of runout on rotating tools and note down measurements above shop limits.
- Do not return damaged tools to the active rack; tag them or store them separately.
Furthermore, record findings in a simple log. The log will determine, over weeks, the tools that are being worn through the quickest, and the operators or machines that are causing the most damage. This information can help with informed purchasing and training decisions.
Proper storage and handling
Carbide is more brittle than hard while still being hard, and if a tool were to fall on the concrete floor or hit another tool, it would chip off immediately. When the tool is not used, the edge is protected by good storage. Utilize dedicated racks, foam inserts, or individual sleeving to prevent contact between cutting edges and metal or other carbide. Do not stack tools loosely in drawers – edges collide with each drawer opening.
The environment matters too. Keep tools in a place where they are not exposed to moisture, as this will cause corrosion on any steel holders and may cause problems in clamping surfaces. Avoid placing tools directly in front of heat sources and where temperature fluctuations are likely to happen. Stable conditions minimize the risk of condensation on tools when they’re removed from the machine.
What is the best way to store carbide tools?
Ideally, carbide tools can be kept in special boxes or free from padding, thus protecting each cutting edge. Additionally, pay attention to keeping them dry, clean, and sorted according to their type and size so that the operators can get them right away. It is important to indicate where every tool must be placed on the rack and return them there after use. Such following of rules allows to avoid confusion and possible damage during rush jobs.
Many workshops buy tools from suppliers like Carbide Tipped Single Point Tools supplier in Dubai and store the devices in their packaging. It is a convenient practice, but keep in mind that once you open the box, you need to organize the tools on a rack that complies with your workflow.
Cutting parameters that extend tool life
The amount of heat and force that reaches the cutting edge is affected by speed, feed, and depth of cut. Too high and the edge becomes soft and hot and wears out rapidly. If they’re too low, the tool rubs rather than cuts, and this can cause built-up edge and poor finish. The intent is to balance the operation and be efficient with removal but not over the edge of the design.
Always use the manufacturer’s recommended data for your material and tool geometry. Then, tune it up slowly, considering sound, chip colour, surface finish, and power consumption. A tool that suddenly sounds harsh or is emitting blue or discolored chips is telling you that heat is building up. A slight decrease in speed is often enough to solve the problem quickly.
Why do speeds and feeds matter so much?
The temperature and load on the cutting edge are controlled by speed and feed, which in turn both affect the tool life. Too fast speeds cause temperatures to get too high, and too high a feed causes the chips to become too thick or stressed. Balanced settings distribute the load on the edge and promote heat removal from the tool by the chip. Generally, it is better to make small, controlled tweaks.
| Parameter | Too High | Too Low | Practical Check |
| Cutting speed | Fast edge wear, thermal cracks | Built-up edge, rubbing | Watch chip color and sound |
| Feed rate | Chipping, edge breakage | Glazing, poor finish | Check surface finish and load |
| Depth of cut | Deflection, vibration | Heat buildup from rubbing | Listen for chatter |
| Stepover (milling) | Overloaded flute | Wasted cycle time | Monitor spindle power |
Record settings that work for each material and tool. A parameter sheet displayed near the machine cuts down on trial and error and ensures consistency of operators from shift to shift.
Coolant and chip control
Coolant has three functions: to cool the cutting zone, to lubricate the area between the tool and the chip, and to remove chips from the cut area. If any of these functions fail, tool life will decrease. Thermal cracking is a frequent problem caused by inconsistent coolant flow, particularly in intermittent cuts where the edge continually heats and cools. Regularly review nozzle alignment, concentration, and filtration.
Chip control is also key. Long stringy chips may wrap around the tool or damage the edge or the workpiece. Flute-packed chips can lead to tool damage. Adjust feed, depth, and coolant pressure to ensure the production of small and sensible chips and clean up chip areas before each setup.
In milling, special attention should be given to flute clearance. Many operators find that by removing the chips between passes from just one flute of the UAE Single Flute Carbide Endmill, the chips are removed more consistently. Where such a coolant is available, it can have a significant impact on these conditions when used through the tool.
- Test the coolant at least once a week using a refractometer.
- Replace or clean filters before they become clogged and cause a restriction in flow.
- Point the nozzles of the aim directly at the cutting area instead of the tool body.
- Use chip breakers or feed rates to adjust chips when they get long and tangled.
- Don’t run dry unless otherwise directed by the tool’s manufacturer.
Resharpening and replacement decisions
Resharpening is only effective if the carbide tool has been worn to a degree that the process can solve the problem and bring the tool back to near-original performance. Typical candidates for light flank wear and edge rounding are minor. Sometimes large chips, deep cracks, and heavy heat damage can be irreparable and cause failure during regrinding. Prior to sending out or grinding in-house, always check the tool.
Regrinding comes with a price tag, and each regrind takes material off the tool. Most carbide cutters can only be reground a finite number of times due to the geometry and the length being shortened. Track regrind counts to prevent the tool from becoming unsafe or inaccurate. A multi-ground tool can still cut, but its tolerance may vary.
Replacement is advisable if the tool is no longer holding size, is not producing the desired finish even at the proper setting, or has cracks that cannot be ground out. Many shops turn to a carbide endmill supplier in Dubai, and they will find that the cost of regrinding compared to new tool prices is a quick decision-making method for them. Reliable suppliers can also determine if a certain geometry needs to be regrinded or not.
How do you know when a carbide tool is finished?
A carbide tool is considered “finished” when it has been adjusted, but it cannot reach the required tolerance, finish, or safety specification. Signs: fast wear, chipping that continuously recurs, increasing spindle load at standard spindle settings, and cracks that can be seen. Have a standardized checklist to make sure this decision is made on facts and not on guesswork. If unsure, remove and check with a new tool.
Maintaining regrind and wear logs will enable you to identify trends. If a specific grade is wearing out too fast on a given material, it might be necessary to use a different grade instead of more frequent replacements. Many shops also use cutting and milling tool suppliers in Dubai to experiment with alternative grades when working on difficult jobs.
However, if you are sending tools to a regrinding service, look for a supplier that has replacements as well. This will assist in changing out a used tool for a new one while not holding up manufacturing. One example of this is that the Saif Precision tools supplier in UAE are often regrinding and restocking their machines in series to minimize machine downtime.
Common mistakes that shorten tool life
A majority of tool failures stem from a handful of predictable errors. The initial step to prevention is recognizing them. Many of the mistakes that occur are not due to lack of care or inexperience by operators, but are due to their haste or lack of direction. They can be eliminated by standard procedures and short training sessions.
- Not using the appropriate grade or geometry of material to be cut.
- Operating a tool equipped with an under-tightened insert or dirty holder pocket.
- Not replacing worn chips, or ignoring early signs of wear, like a change in sound.
- Loosely storing tools where edges meet.
- Waiting to detect a problem before getting the coolant checked.
- Excessive clamping force on clamp screws, causing cracks in inserts or pockets.
- Spending a lot on a tool but not investing the time to regrind it because it’s cheaper in the short term.
Don’t rush to complete the next part with a tool. When cutting with a worn edge, an extra pass may cause damage to the edge as well as to the workpiece. It is nearly always cheaper to stop early and replace or regrind the tool than it would be to recover from a crashed insert or from a ruined part.
Choosing a reliable tool supplier
Proper tools are crucial for maintenance processes. A trustworthy supplier makes sure that the tool possesses good quality, accurate information about it, and provides quick tool replacements when necessary. The supplier should be able to give information about cutting angles, shapes, and requirements regarding parameters, not just inform about prices. A good supplier is ready to help with resolving issues connected with tools that work improperly.
Moreover, check out the products offered. The supplier should offer different types of tools, thus making the purchasing easier and allowing the company to work with fewer suppliers. Besides, by cooperating with one supplier, the workers will have the chance to learn about the tools more thoroughly and make sure that they can use the data everywhere.
Last but not least, find out what after-sales service the supplier offers. It is necessary to know whether there is a possibility to regrind, get advice on the use of tools, or get samples for testing.
What should you look for in a tool supplier?
Search for a supplier that guarantees the quality of products, whose technical documentation is clear and comprehensive, and that has a reputation among machine shops operating in the area. A supplier of Carbide Tipped Single Point Tools in Dubai must have the ability to communicate information about insert grades, geometry choices, and recommendations on cutting conditions in non-technical terms.
Equally, timely and efficient communication and the capability of prompt delivery are essential when the assembly line is waiting for the supplies. Before making a large order, try to test the supplier’s reliability by placing a minimal order first.
Conclusion
Carbide tool maintenance isn’t an easy task; however, it requires regularity. Inspection daily, proper storage, accurate cutting parameters, consistent cooling rate of coolants are important for extending tool life and maintaining parts quality. Those machinists who develop good habits during their shifts have less waste, fewer breakdowns, and more predictable costs. Begin with one or two practices for this week; then measure their effectiveness before expanding further.
Furthermore, working together with an experienced Carbide Tipped Single Point Tool provider in Dubai, or another reputed vendor, helps you maintain your equipment at peak performance levels while ensuring timely completion of projects. Visit almifthaah to explore tooling options and plan your next restock.
Frequently asked questions
Check carbide tools during each shift and also when there is an issue with part quality. Visual inspection is quick to detect chips, cracks, and loose inserts before they cause damage.
Yes, many carbides are recyclable for multiple uses; however, each grinding process removes some amount of metal from them. Monitor the regrind count, and decommission the tool if it becomes too low or loses tolerance.
Chipping is caused by overfeeding, instability of equipment, loose inserts, and rough handling. Reducing rigidity and checking parameters usually results in a significant reduction of chipping.
Yes, coolant controls temperature, lubricates cuts, and improves chip clearance. Thermal cracking and early edge failures are often caused by inconsistent or poor cooling efficiency.
How to Identify the Correct Gear Cutter When the Markings Are Missing
Carbide Tool Maintenance Tips Every Machinist Should Know