- October 19, 2026
- by Almifthaah
How to Select an Involute Gear Cutter by Module and Number of Teeth
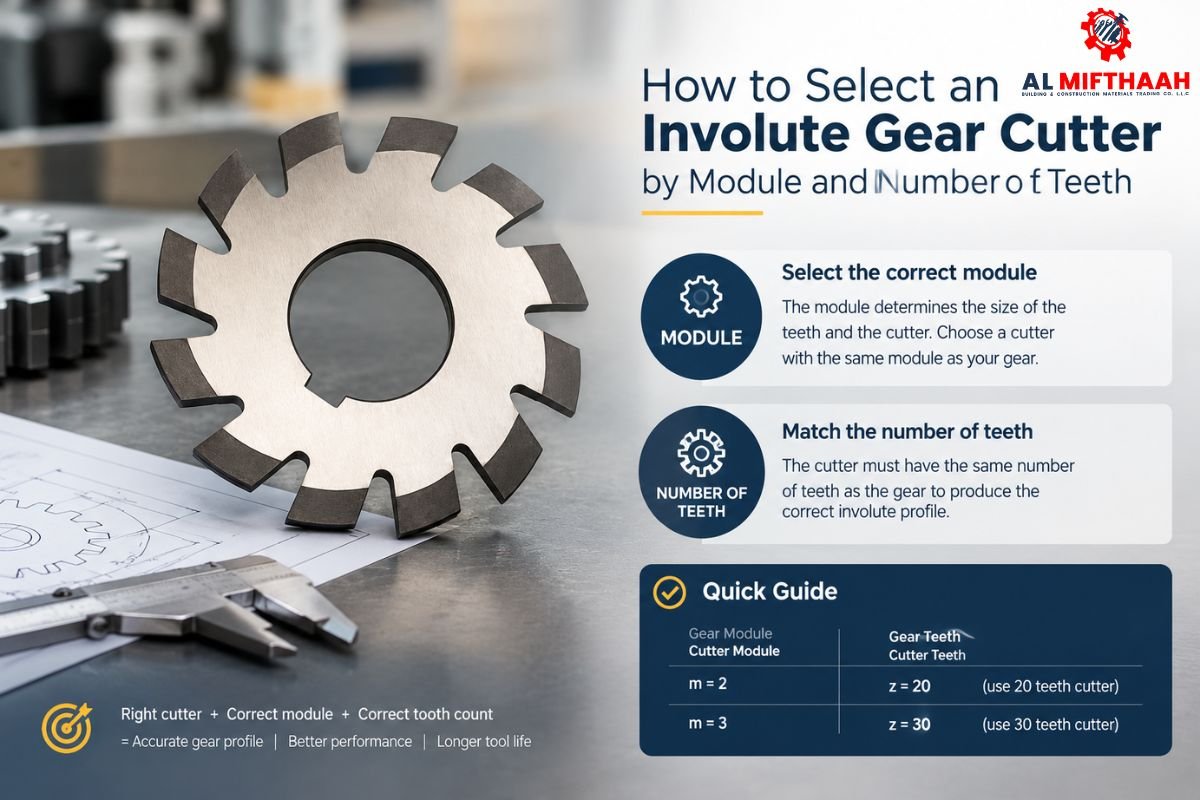
Selecting an involute gear cutter requires determining the gear’s module and pressure angle, then determining how many teeth the gear has, before picking a cutter whose number includes that number of teeth. The module is what determines the size of the teeth, while the number of teeth determines the profile of the cutter.
Making an error in any of these processes will result in the gear being cut, but it will not be able to contribute to meshing. This means backlash, binding teeth, noise, and accelerated wear. This guide deals solely with spur gears produced by means of a milling machine equipped with a form cutter and is aimed at the process of choosing a cutter, as well as giving an example of the correct procedure.
Table of Contents
ToggleKey takeaways
- Both the module and the pressure angle must be exactly the same as those of the gear. There is no room for ‘close enough’ here.
- The cutter you need depends on how many teeth the gear has.
- Each cutter can cut a certain range of tooth counts, not just a single count.
- Before you start cutting, always check the cutter markings, not after.
What does module mean on a gear cutter?
Module is the pitch diameter divided by the number of teeth, in millimetres. A module 3 gear has 3 mm of pitch diameter for every tooth. A bigger module means bigger teeth.
A module gear cutter is ground to one module only. A module 2 cutter cannot cut a module 2.5 gear, even though the difference looks small on paper.
Some quick relationships help when you size up a gear:
- Addendum (tooth height above the pitch circle) equals 1 × module
- Dedendum (below the pitch circle) is typically 1.25 × module
- Whole depth is therefore about 2.25 × module
- Outside diameter of the blank is module × (teeth + 2)
However, if your drawing gives diametral pitch instead, convert it: module = 25.4 ÷ DP. Mixing the two systems is one of the easiest ways to order the wrong cutter.
Why does the number of teeth change the cutter?
This surprises many people. Two gears with the same module can have different tooth shapes if their tooth counts differ.
An involute curve is generated from the base circle. A small gear has a smaller base circle, so its tooth flank curves more sharply. A large gear has a flatter flank, and a rack (infinite teeth) has straight sides.
So an involute gear cutter cannot use one shape for every gear. The tooth space it leaves has to match the gear being cut. That is why a standard set contains several cutters per module, and why the gear cutter number of teeth matters as much as the module. Consulting the milling cutter dealers in Dubai can be helpful.
How do cutter numbers map to tooth counts?
The common arrangement is a set of eight cutters, numbered 1 to 8. Together they cover gears from 12 teeth up to a rack.
| Cutter No. | Tooth range it covers |
| 1 | 135 to rack |
| 2 | 55 to 134 |
| 3 | 35 to 54 |
| 4 | 26 to 34 |
| 5 | 21 to 25 |
| 6 | 17 to 20 |
| 7 | 14 to 16 |
| 8 | 12 to 13 |
Wait, that ordering needs care. Numbering conventions are not universal. Many sets run No. 1 for the smallest tooth counts and No. 8 for the largest, and others run the other way. Always read the range printed on the cutter or the manufacturer’s chart instead of trusting memory.
For reference, here is the more widespread layout, where No. 1 cuts the fewest teeth:
| Cutter No. | Teeth it cuts |
| 1 | 12 to 13 |
| 2 | 14 to 16 |
| 3 | 17 to 20 |
| 4 | 21 to 25 |
| 5 | 26 to 34 |
| 6 | 35 to 54 |
| 7 | 55 to 134 |
| 8 | 135 to rack |
Furthermore, each cutter is shaped for the smallest tooth count in its range, so profile accuracy is best there and drifts slightly toward the top of the range. For ordinary workshop and maintenance gears, that small difference is acceptable. For gears running at high speed or carrying heavy load, ask whether a finer set with half-number cutters is available.
Does pressure angle matter?
Yes. Pressure angle is the angle between the line of force on the tooth and the direction of motion at the pitch point. It controls tooth thickness at the root and how the flanks contact.
Two angles show up most often:
- 20 degrees: the standard for modern module gears
- 14.5 degrees: an older standard, still found on legacy machinery
Gears only mesh correctly when both have the same pressure angle. A 20-degree cutter used on a 14.5-degree gear leaves the wrong flank shape. The pair may turn by hand and still fail under load. If you are replacing a gear on old equipment, measure or check the original drawing before assuming 20 degrees. Cutting and milling tools Dubai will be beneficial.
How to select a gear cutter step by step?
Work through these in order. Skipping ahead is where most errors begin.
- Confirm the module: Use the drawing. If you are copying an existing gear, measure the outside diameter and count the teeth, then work backward: module = OD ÷ (teeth + 2).
- Confirm the pressure angle: Check the drawing or the mating gear.
- Count the teeth: Use the gear’s final tooth count, not an approximation.
- Pick the cutter number: Match the tooth count to the cutter range on the set chart.
- Check bore and diameter: The cutter bore must fit your arbor, and the cutter’s outside diameter must clear your setup.
- Check the material: High-speed steel is the usual form-cutter material. Confirm the cutter suits your blank, whether steel, cast iron or brass.
- Verify the markings: Module, pressure angle, and cutter number should all be visible on the cutter face.
Worked example: module 3 gear pair
Say you need a pinion with 18 teeth and a mating gear with 54 teeth. Both are module 3, 20 degrees pressure angle, spur type.
Pinion (18 teeth)
- Pitch diameter: 3 × 18 = 54 mm
- Blank outside diameter: 3 × (18 + 2) = 60 mm
- Cutter: module 3, 20 degrees, No. 3 (17 to 20 teeth)
Gear (54 teeth)
- Pitch diameter: 3 × 54 = 162 mm
- Blank outside diameter: 3 × (54 + 2) = 168 mm
- Cutter: module 3, 20 degrees, No. 6 (35 to 54 teeth)
Shared figures
- Whole depth: 2.25 × 3 = 6.75 mm
- Centre distance: 3 × (18 + 54) ÷ 2 = 108 mm
Notice that 54 teeth sit right at the top of the No. 6 range. The cutter is shaped for 35 teeth, so the profile is a touch off at 54. For a general-purpose gear, this is fine. If the drive is critical, ask about a half-number cutter, and gear cutters dealers in Dubai can help you.
Common selection mistakes and how to avoid them
- Ordering by module alone- A module 3 cutter set has eight cutters. Buying “a module 3 cutter” without a number is incomplete.
- Mixing module and DP- A 10 DP gear is module 2.54, not module 2.5. Convert properly before ordering.
- Ignoring pressure angle- Always confirm it, especially on older equipment.
- Choosing by blank size- Outside diameter tells you about the gear, but the tooth count decides the cutter.
- Assuming the whole set is needed- If you are cutting gears with a single tooth count, one cutter is enough. Buying the full set only makes sense when you cut a range of sizes.
- Using the wrong cutter for helical gears- Straight-form cutters are matched to spur gears. Helical gears behave differently because the tooth shape in the cutting plane depends on the helix angle. Treat that as a separate selection task.
- Skipping the arbor check- A cutter with the wrong bore or keyway wastes time and can damage the arbor.
What to check when buying locally in Dubai?
If you are sourcing through gear cutters suppliers in Dubai, a clear enquiry saves days. Send the supplier:
- Module (or DP, with the conversion confirmed)
- Pressure angle
- Number of teeth, or the cutter number you need
- Bore size and keyway
- Cutter material
- Single cutter or full set
Local availability matters because cutter sets for common modules are often needed quickly on maintenance jobs. Many workshops compare gear cutter dealers in Dubai for lead time as much as price. The same suppliers often carry cutting and milling tools Dubai buyers need alongside the gear cutter, such as arbors and end mills.
Almifthaah, also known as Saif Precision tools supplier in UAE, works in precision tools and abrasives. If you are comparing milling cutter dealers in Dubai, send your module, pressure angle, and tooth count so the right cutter number can be confirmed before you order.
Final thoughts
Selecting an involute gear cutter comes down to three confirmed numbers: module, pressure angle, and tooth count. Module and pressure angle must match the gear exactly. The tooth count then points you to the right cutter number.
Read the range on the cutter, check the bore, and use a half-number cutter when accuracy matters at the edge of a range. When you contact gear cutters suppliers in Dubai, send the full specification in your first message. It saves a round of emails and lowers the chance of the wrong cutter arriving.
Frequently asked questions
It is a form milling cutter with an involute tooth profile. Fed into a gear blank, it cuts one tooth space at a time.
Match the module printed on the drawing or measured from the gear. The cutter module must be identical to the gear module.
Each cutter covers a range. A standard set of eight covers 12 teeth up to a rack.
Module is in millimetres of pitch diameter per tooth. Diametral pitch is teeth per inch. Module equals 25.4 divided by DP.
No. The pressure angles must match, or the flank shape will be wrong, and the gears will mesh poorly.
Only if you cut a wide range of tooth counts. For one gear, a single correct cutter is enough.
Measure the outside diameter, count the teeth, then divide the diameter by teeth plus two.
No. The cutter number identifies a range. You need to read the chart to match it to your tooth count.
High-speed steel is the most common for form cutters used in workshop milling.
Module, pressure angle, cutter number, bore, keyway, and material. Confirm all of them in writing.
How Thick Should Copper Shim Stock Be for Electrical Busbar Connections?
How to Select an Involute Gear Cutter by Module and Number of Teeth